

News
Unleashing the Power of Halogen Moisture Analyzers for Quality Control in the Chemical Industry
2025-02-25
Unleashing the Power of Halogen Moisture Analyzers for Quality Control in the Chemical Industry
Table of Contents
- 1. Introduction to Halogen Moisture Analyzers
- 2. The Importance of Quality Control in the Chemical Industry
- 3. How Halogen Moisture Analyzers Work
- 4. Benefits of Using Halogen Moisture Analyzers
- 5. Applications in Industrial Chemical Manufacturing
- 6. Choosing the Right Halogen Moisture Analyzer
- 7. Best Practices for Moisture Analysis
- 8. Future Trends in Moisture Analysis Technology
- 9. Frequently Asked Questions
- 10. Conclusion
1. Introduction to Halogen Moisture Analyzers
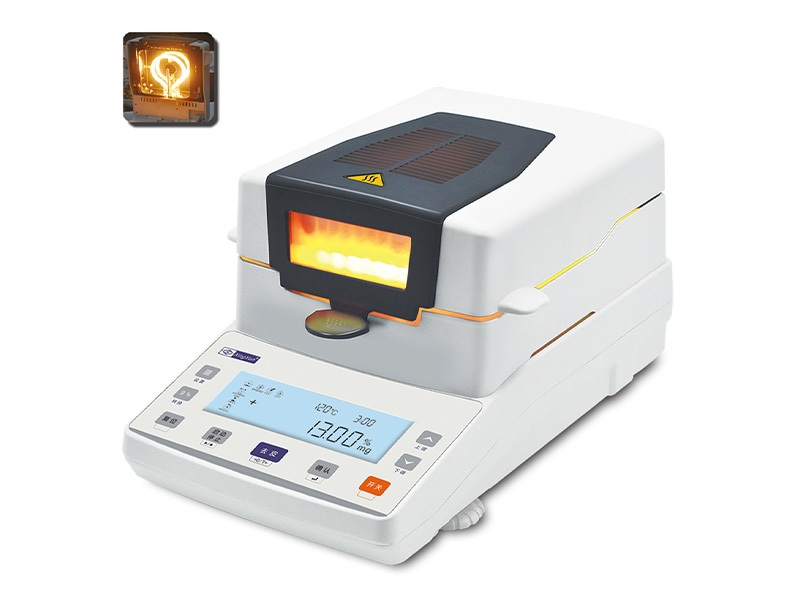
In the quest for maintaining quality in the chemical industry, the role of moisture analyzers has become paramount. Among the various types of moisture analyzers available, halogen moisture analyzers stand out due to their speed, accuracy, and efficiency. These instruments utilize halogen lamps to heat samples and determine moisture content rapidly, making them essential for quality control processes.
2. The Importance of Quality Control in the Chemical Industry
Quality control is not just a regulatory requirement; it is the backbone of the chemical industry. Ensuring that products meet stringent specifications can prevent costly recalls and maintain customer trust. Moisture control is critical as it affects product stability, shelf life, and overall performance. Therefore, effective moisture measurement is indispensable for maintaining quality and compliance.
3. How Halogen Moisture Analyzers Work
Halogen moisture analyzers operate through a straightforward yet sophisticated process. The sample is weighed before and after heating with halogen light. The moisture evaporates, and the loss in weight is calculated to provide precise moisture content. The rapid heating capability of halogen lamps significantly reduces testing time, making it a favorite among manufacturers who require quick results without compromising accuracy.
3.1 The Heating Process
Halogen lamps emit infrared radiation, which heats the sample uniformly. This process ensures that moisture is released efficiently, allowing for rapid analysis. The temperature can be precisely controlled, ensuring consistency across tests.
3.2 Weight Measurement
Most halogen moisture analyzers come equipped with high-precision balances, which measure the weight loss with extreme accuracy. This dual functionality allows for seamless transitions from heating to measurement, thereby increasing operational efficiency.
4. Benefits of Using Halogen Moisture Analyzers
The adoption of halogen moisture analyzers in the chemical industry offers numerous benefits that enhance the quality control process.
4.1 Speed and Efficiency
One of the main advantages of halogen moisture analyzers is their rapid testing capabilities. Traditional methods can take hours, while halogen methods can provide results in just a few minutes.
4.2 Precision and Accuracy
These analyzers deliver highly accurate results, often with a precision of 0.01%. This level of accuracy is crucial for industries where even minute variations in moisture content can affect product quality.
4.3 User-Friendly Interface
Modern halogen moisture analyzers are designed with user-friendly interfaces that simplify operation. The digital displays often provide real-time results and allow users to set specific parameters for their tests.
4.4 Versatility
Halogen moisture analyzers are versatile tools that can be used for a wide range of materials, including powders, granules, and liquids, making them applicable across various chemical manufacturing processes.
5. Applications in Industrial Chemical Manufacturing
Halogen moisture analyzers find applications in multiple sectors within the chemical industry.
5.1 Polymer and Plastics Industry
In the production of polymers, moisture content is critical as it can affect polymerization processes. Halogen moisture analyzers are used to ensure optimal moisture levels for high-quality products.
5.2 Pharmaceutical Manufacturing
Moisture analysis is vital in pharmaceutical manufacturing. Ensuring that active ingredients remain stable throughout production and storage is crucial, and halogen analyzers provide quick and reliable measurements.
5.3 Food and Beverage Chemistry
The food industry also relies on halogen moisture analyzers for ensuring the quality and safety of products. Accurate moisture control helps prevent spoilage and maintains product integrity.
6. Choosing the Right Halogen Moisture Analyzer
Selecting the appropriate moisture analyzer involves several considerations to meet specific industry needs.
6.1 Understanding Your Requirements
Before purchasing a halogen moisture analyzer, it is essential to understand the material being tested and the moisture content range required. Different models cater to varying needs, and identifying these factors can help in making an informed choice.
6.2 Budget Considerations
While investing in high-quality equipment is necessary, it is also important to consider the budget. Compare the features and benefits of various models to find one that offers the best value for your investment.
6.3 Manufacturer Support and Warranty
Choose a manufacturer that provides excellent customer support and a comprehensive warranty. This ensures that your investment is protected and that help is readily available should any issues arise.
7. Best Practices for Moisture Analysis
To achieve optimal results with halogen moisture analyzers, following best practices is essential.
7.1 Calibration and Maintenance
Regular calibration and maintenance of the analyzer are crucial to ensure accuracy. Follow the manufacturer’s guidelines for maintenance schedules and procedures.
7.2 Sample Preparation
Proper sample preparation can significantly impact the accuracy of moisture readings. Ensure samples are representative and prepared according to the analyzer’s specifications.
7.3 Data Interpretation
Understanding how to interpret the data generated by halogen moisture analyzers is vital. Familiarize yourself with the software and reporting features to make informed decisions based on the results.
8. Future Trends in Moisture Analysis Technology
As technology continues to evolve, we can expect significant advancements in moisture analysis.
8.1 Integration with IoT
The integration of IoT (Internet of Things) technology in moisture analyzers will allow for remote monitoring and real-time data analysis, enhancing operational efficiency.
8.2 Enhanced Automation
Future models may incorporate more automated features, reducing the need for manual input and increasing the consistency of results.
8.3 Advanced Data Analytics
The future will likely see the implementation of advanced data analytics capabilities, allowing for deeper insights into moisture trends and better decision-making processes.
9. Frequently Asked Questions
9.1 What is a halogen moisture analyzer?
A halogen moisture analyzer is a device that uses halogen lamps to quickly and accurately measure the moisture content in various materials.
9.2 How does a halogen moisture analyzer work?
It works by heating a sample with halogen light, causing moisture to evaporate, and then weighing the loss to determine moisture content.
9.3 What are the benefits of using halogen moisture analyzers?
They offer speed, accuracy, ease of use, and versatility across different materials.
9.4 In which industries are halogen moisture analyzers commonly used?
They are widely used in the polymer, pharmaceutical, and food industries for quality control.
9.5 How often should a halogen moisture analyzer be calibrated?
Calibration frequency depends on usage, but regular checks are essential to maintain accuracy.
10. Conclusion
Halogen moisture analyzers are transforming quality control processes in the chemical industry. By offering rapid and accurate moisture measurements, they ensure that products meet strict quality standards while enhancing operational efficiency. As the industry continues to evolve, adopting advanced moisture analysis technology will be crucial for maintaining competitive advantage and ensuring product quality. Embracing these innovative tools will not only lead to better quality control but also pave the way for a more reliable and efficient chemical manufacturing process.
Related News


Copyright © 2023 Changzhou Xingyun Electronic Equipment Co.,Ltd. Powered by:www.300.cn Tags
Business License